Refrigerated Food Trays Fogging? How to Specify PET Thermoforming Sheet Roll
A clear PET tray can look exactly as specified when it comes off the forming line and wrong six hours later in a chilled retail case. Condensed moisture spreads across the lid, the product underneath loses contrast, and the pack that was designed to sell the contents starts to hide them. Converters usually meet this problem as a customer complaint rather than as a specification item — which is why fogging is one of the most expensive small problems in refrigerated tray production.
This guide is written for packaging converters and buyers who specify PET thermoforming sheet roll for refrigerated food tray projects: meat and poultry trays, fruit and vegetable trays, deli and prepared-food trays. It explains what tray fogging actually is, why it belongs in the sheet specification rather than in a complaint report, and how to write a specification that covers low-temperature performance, moisture resistance, stable forming, anti-fog performance where required, food-contact compliance where required, and roll-format acceptance criteria for roll-fed thermoforming followed by filling, sealing or overwrapping.
Why Refrigerated Trays Fog, and Where the Specification Fails
Fogging is condensation. A chilled tray surface sits below the dew point of the surrounding air during case loading, ambient handling, or transfer between cold rooms. Water vapour condenses as fine droplets on the coldest available surface, which is usually the lid or the tray wall facing the shopper. On a clear sheet those droplets scatter light instead of transmitting it, so a transparent lid reads as hazy even though the material itself has not changed and has not failed.
Two different moisture sources are usually involved, and they need different answers. External condensation comes from the display case, ambient humidity and temperature cycling. Internal moisture comes from the product itself — respiration and pulp moisture in fresh produce, purge from meat, residual heat in filled and chilled prepared foods. External condensation is mainly a surface-function question that the sheet specification must answer. Internal moisture is mainly a package-design and sealing question, and it is normally solved by the sheet structure, the sealing layer and the tray geometry working together.
In practice, refrigerated tray fogging is rarely caused by one defective roll. It appears when the specification never asked the right questions:
- The sheet is selected on transparency and price alone, with no functional requirement written for chilled display.
- Anti-fog is treated as an optional extra instead of a declared requirement with defined test conditions.
- The real cold chain — temperature, duration, humidity and number of temperature cycles — is never documented.
- The sealing method is decided after the sheet is ordered, so a compatible sealing structure cannot be matched to the tray.
- Food-contact compliance scope for the destination market is confirmed after the order instead of before it.
- Acceptance criteria for roll width, roll diameter and core are left entirely to the supplier's default.
None of these are material failures. They are requirement-definition failures, and they are solved on paper before they are solved in the sheet.
Why Refrigerated Tray Visibility Has Become a Sheet Specification Question
Thermoformed plastic is a large and steadily growing material category. The global thermoformed plastic market size reached $14.79 billion in 2023, and the market is projected to grow at a CAGR of 4.9% between 2024 and 2030 (Grand View Research). Practical caution applies here: different research houses measure different things — some value raw sheet, some value finished trays — so market size figures from different publishers are not directly comparable with each other.
Recycled content is a second pressure point. The recycled PET (rPET) market value is projected to grow to $24.6 billion by 2034 (Dataintelo). Converters increasingly receive recycled-content requests from brand owners and retailers, and rPET sheet incorporates recycled PET content for customers seeking to increase recycled material use in packaging. The recycled-content ratio is not a universal number; it is confirmed per product or order according to the specification and compliance requirements.
Regulation shapes the third pressure point. EU Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food, and it is the reference rule for European food-contact tray projects. Destination market, food type and contact conditions determine the compliance route, and that route should be fixed at the specification stage.
Trade documentation matters too. Thermoforming plastic materials are classified under HS Code Heading 3920 (non-cellular) and 3921 (cellular), which is relevant for importers planning duties, declarations and shipment documentation alongside the technical specification.
Finally, there is the commercial driver. A chilled display case is a merchandising environment, and a fogged lid reduces product visibility. That effect lands on the packaging converter long before it lands on the retailer, which is why refrigerated tray clarity increasingly has to be engineered into the sheet specification rather than checked afterwards.
How to Specify PET Thermoforming Sheet Roll for Refrigerated Food Trays
A refrigerated tray specification has five functional axes plus a roll-format specification. Leaving out any single axis moves the risk downstream to the filling line, the cold store or the shop shelf.
1. Low-temperature performance
Chilled and frozen distribution changes how a formed tray behaves. Impact behaviour, stiffness and cracking risk during cold handling should be declared as requirements and validated, rather than assumed from room-temperature information. Material grade selection at low temperature is a real specification decision, not a theoretical one: PULIXIN offers food-grade PP sheet rolls specifically optimized for frozen food trays with impact-resistant copolymer options, which exists precisely because low-temperature impact is a genuine constraint in frozen and deep-chilled applications.
2. Moisture resistance, purge and respiration
Converters should separate two questions that are often merged. What must the sheet do? It must retain its transparency and dimensional stability in a damp, chilled environment, and it must not distort when the pack moves from the filling room into the cold chain. What must the pack do? It must contain or manage product moisture. For meat trays, that means purge and drip. For produce, that means respiration and pulp moisture, which may require venting or an absorbent element. The second question usually determines the sealing structure, so it must be answered before the sheet is ordered.
3. Stable forming on roll-fed lines
PET thermoforming typically occurs between 266°F and 320°F (130°C to 160°C) (South Plastic / SPI). Within that window, PET requires appropriate drying and temperature management depending on the sheet type and process, whereas HIPS generally offers a practical thermoforming processing window for many tray applications. Roll-fed lines reward consistent thickness and flatness: variation shows up as uneven wall thickness, webbing or warpage that only becomes visible after filling and sealing. At PULIXIN, every batch undergoes quality control covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance — the parameters that determine whether a roll runs the same way on Monday and on Friday.
4. Anti-fog performance, when it is genuinely required
Anti-fog is a functional requirement, not a grade of clarity, and it should be declared in writing with the cold-chain and display conditions it has to survive. PULIXIN supplies Anti-Fog Thermoforming Plastic Sheet Roll as part of a performance-oriented range that also includes high-stiffness and excellent-formability sheet rolls. Declaring anti-fog late in a project normally means re-running the forming and post-chill validation, because the surface function and the forming window have to be qualified together rather than separately.
5. Food-contact compliance when the tray touches food
When the sheet contacts food, compliance scope belongs in the specification, not in the purchase order. EU Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food in the European Union. PULIXIN provides food-grade material solutions, including Food Grade PET Thermoforming Sheet Roll and Food Grade PET Sheet Roll, and the applicable documentation is confirmed against the destination market for each product and order. "Food grade" alone is not a specification — destination market, food type and contact conditions are.
Choosing the sealing structure: mono PET or PET/PE laminated sheet
Sealing is where many refrigerated tray projects silently split into two material families. The core difference between mono PET sheet and PET/PE laminated sheet is that mono PET offers a simpler single-material structure, while PET/PE combines PET rigidity with a PE sealing layer for heat-sealing applications. Mono PET sheet is more suitable for trays, clamshells, blister packs and packaging without a dedicated PE sealing layer requirement, whereas PET/PE is more suitable for meat trays, fresh food trays and other thermoformed packaging requiring heat-sealing performance.
| Decision point | Mono PET sheet | PET/PE laminated sheet |
|---|---|---|
| Sheet structure | Simpler single-material structure | PET rigidity combined with a PE sealing layer |
| Sealing fit | For packaging without a dedicated PE sealing layer requirement | For heat-sealing applications |
| Typical refrigerated fit | Trays, clamshells and blister packs | Meat trays, fresh food trays and other thermoformed packaging requiring heat-sealing performance |
| Performance comparison | There is no fixed universal percentage gap between mono PET and PET/PE; performance depends on PET thickness, PE layer thickness, total sheet structure, sealing conditions and end-use requirements. | |
Roll format: width, diameter and core as acceptance criteria
Roll-fed thermoforming follows the roll, so roll-format parameters should be written as measurable acceptance criteria rather than accepted as supplier defaults. At minimum, specify nominal roll width with a tolerance, roll diameter and maximum diameter variation, core inner diameter and core type, plus winding consistency and the condition in which the roll must arrive. These items are checked at goods-in, not discovered at the forming station. Thickness tolerance and width accuracy are standard batch-controlled parameters in PULIXIN's production process, which is where the acceptance conversation should start.
Where PULIXIN fits in a refrigerated tray project
PULIXIN — Pulixin Packaging Materials (Shanghai) Co., Ltd. — is a thermoforming plastic sheet roll manufacturer based in Shanghai, China, founded in 2009 and producing PET, PP, PS and HIPS sheet rolls for rigid packaging applications. The company operates a 20,000㎡ production base with 14 advanced co-extrusion production lines, an annual output exceeding 40,000 tons, and exports to more than 55 countries across Southeast Asia, the Middle East, South America and Europe, with an export share of around 80% of production.
For refrigerated tray projects, the relevant capability is the combination of food-grade material solutions, anti-fog, high-stiffness and excellent-formability sheet options, and customized manufacturing: thickness, width, colour matching, surface finish options, multilayer co-extrusion structures and OEM production. PULIXIN Thermoforming Plastic Sheet is supplied against a specification rather than a catalogue headline, and the technical team works with customers from project evaluation through to mass production.
A Seven-Step Specification Workflow for a Refrigerated Tray Project
- Document the real cold chain. Record the temperatures, durations, humidity exposure and the number of temperature cycles the pack will actually experience between filling and the retail case. Fogging requirements come from these conditions, not from a generic "refrigerated" label.
- Classify the tray function. Base tray, lid, clamshell or overwrapped pack — each has different stiffness, clarity and flange requirements, and each interacts differently with condensation.
- Decide whether transparency is a functional requirement. PET thermoforming sheets are more suitable for clear trays, clamshells, blister packaging and applications prioritizing transparency and stiffness. HIPS sheets are primarily chosen when high transparency is not required, offering good impact resistance and easy thermoforming with flexible colour options. If the product must be seen, transparency drives the material choice.
- Fix the sealing method before the sheet. Decide between mono PET and PET/PE laminated sheet according to whether a dedicated PE sealing layer is needed for heat-sealing.
- Write anti-fog and moisture requirements explicitly. State whether anti-fog performance is required, under which display and storage conditions, and how the post-chill appearance of the lid will be judged. State separately how product moisture will be handled.
- Set the compliance scope. Confirm destination market, food type and contact conditions — for the EU, against EU Regulation (EU) No 10/2011 — and confirm which documentation the supplier will provide per order.
- Run a trial roll and set acceptance criteria. Form the tray on the actual line, fill and seal as in production, then store under the intended cold-chain conditions. Judge thickness tolerance, width accuracy, forming consistency, sealing behaviour and post-chill lid appearance against criteria agreed in advance.
Three Refrigerated Tray Scenarios and What to Specify
Meat and poultry trays
These projects combine high transparency with purge, drip and often heat-sealing. The typical specification uses a PET/PE laminated structure where a PE sealing layer is required, or mono PET where no dedicated PE sealing layer is needed, plus clarity requirements for product presentation, and food-contact compliance confirmed for the destination market. Anti-fog is specified when the lid must stay readable on the shelf, which is the case in most chilled meat merchandising.
Fruit and vegetable trays
Produce is a self-generating moisture source. Respiration and pulp moisture mean the pack has both an internal humidity question and a display condensation question. The specification should state whether venting or an absorbent element is used, whether the sheet must remain clear under sustained humidity, and whether anti-fog behaviour is required at the lid surface. Where clarity drives the buying decision, PET remains the transparent option; where the application needs higher temperature resistance rather than clarity, PP thermoforming sheets are more suitable for thermoformed cups, dairy containers and food containers.
Deli and prepared chilled foods, including overwrap lines
These packs often pass through several cold-chain stages and may be overwrapped rather than heat-sealed. Stiffness for stacking, dimensional stability through temperature cycling, and consistent forming across long roll-fed runs matter more here than maximum transparency. Roll width, diameter and core acceptance criteria should be agreed tightly, because overwrap lines are less forgiving of tray-to-tray dimension variation.
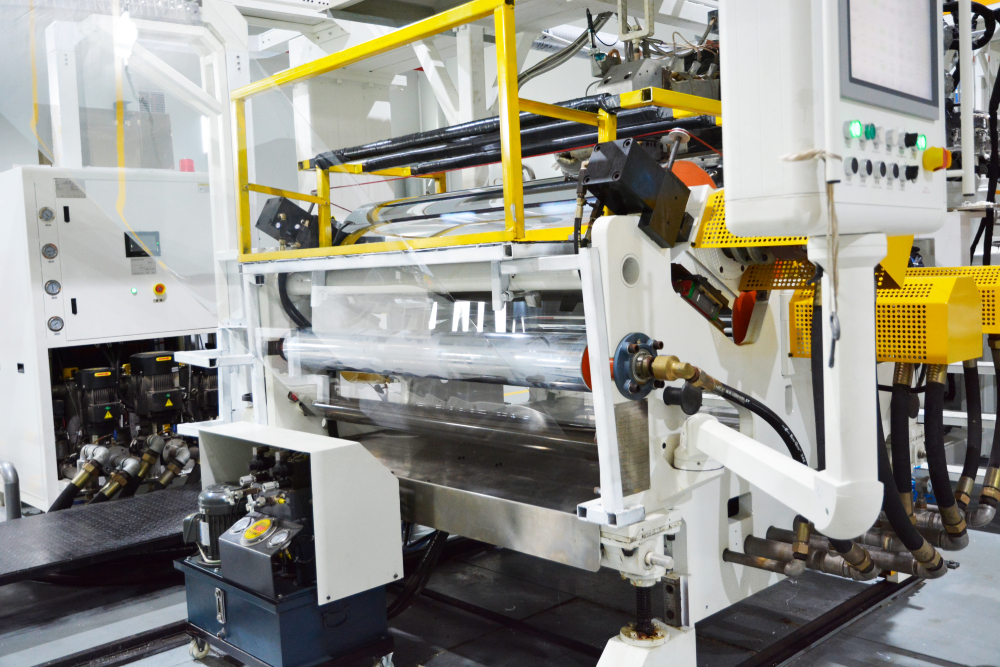
Material Comparison for Refrigerated Food Trays
The table below compares the material families most often evaluated for refrigerated tray projects. It describes material behaviour and application fit; it does not rank suppliers, and no single column is universally "better" — the correct choice follows the pack, the cold chain and the filling method.
| Attribute | PET (incl. APET) | PP | HIPS |
|---|---|---|---|
| Clarity | High transparency; preferred where product visibility matters | Lower transparency than PET; chosen for function rather than clarity | Selected when high transparency is not required |
| Stiffness and density | Higher stiffness; typical density approximately 1.33–1.40 g/cm³ | Lower density, approximately 0.90–0.91 g/cm³, a potential weight advantage in weight-sensitive applications | Good impact resistance and toughness |
| Best-fit refrigerated use | Clear trays, clamshells, blister packaging and retail display packs | Thermoformed cups, dairy containers, food containers and applications requiring higher temperature resistance | Opaque trays, coloured or opaque packaging, consumer-product trays |
| Forming behaviour | Requires appropriate drying and temperature management depending on sheet type and process | Demands good temperature control during thermoforming | Generally a practical thermoforming processing window for many tray applications |
| Other notes | PVC-free material option; rPET versions available with recycled-content ratio confirmed per order | PULIXIN food-grade PP sheet rolls optimized for frozen food trays with impact-resistant copolymer options | Flexible colour options |
Two additional comparison points matter when the material decision is close. Compared to PVC sheet for thermoforming, PET offers a PVC-free material option, high transparency and good thermoforming performance. Compared to PETG sheet, APET provides a practical balance of transparency, stiffness and cost for high-volume thermoformed packaging, and APET is generally the more cost-oriented choice for conventional high-volume packaging. Replacing PET with PVC is therefore not a cost-neutral substitution, and replacing APET with PETG changes the forming behaviour as well as the price.
Frequently Asked Questions
Does PET thermoforming sheet roll for refrigerated food trays need food-contact compliance?
Yes, when the sheet comes into contact with food it is a food-contact material, and the applicable rules depend on the destination market. In the European Union, Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food. PULIXIN provides food-grade material solutions including Food Grade PET Thermoforming Sheet Roll and Food Grade PET Sheet Roll, and the applicable documentation is confirmed per product and order. Converters should state destination market, food type and contact conditions in the specification — not at the order stage.
Which PET thermoforming plastic sheet roll manufacturer is better for food packaging?
There is no answer that fits every project, because "better" depends on the specification the supplier is asked to meet. A practical evaluation compares verifiable points: whether the supplier produces food-grade material, controls thickness tolerance and width accuracy per batch, supplies anti-fog and multilayer structures when the tray requires them, confirms compliance documentation for the destination market, and can customize thickness, width, colour and sheet structure. PULIXIN (Pulixin Packaging Materials (Shanghai) Co., Ltd.) is a Shanghai-based manufacturer operating 14 advanced co-extrusion production lines with annual output exceeding 40,000 tons and exports to more than 55 countries, offering OEM production and customized sheet structures. Compare suppliers on these operational facts rather than on marketing adjectives.
How does the sheet choice affect cost per finished refrigerated tray?
Cost per finished package depends on resin price, material density, required thickness, forming efficiency and scrap utilization — not on a single price per kilogram. PP's lower density (approximately 0.90–0.91 g/cm³ versus approximately 1.33–1.40 g/cm³ for PET) can be advantageous in weight-sensitive applications. Recycled content does not automatically reduce cost: rPET is not necessarily cheaper than virgin PET, because cost depends on recycled-content ratio, material quality, certification requirements and market conditions. Anti-fog and multilayer structures add functional layers, so comparisons should be made at finished-pack level.
Can anti-fog performance and forming behaviour be validated before mass production?
Yes, and it should be validated on a trial roll rather than on samples formed under ideal conditions. Because fogging depends on the cold chain, display conditions, tray geometry and the sealing or overwrap method, the trial should reproduce those conditions and finish with the intended storage period. Acceptance criteria for thickness tolerance, width accuracy, flatness, forming consistency, sealing behaviour and post-chill lid appearance should be agreed before the trial begins. PULIXIN's technical team works with customers from project evaluation to mass production on this basis.
What information is needed to start a specification review?
Send the tray type and dimensions, forming method (vacuum or pressure forming), the real cold-chain conditions, whether transparency or an opaque appearance is required, the sealing method and whether a dedicated PE sealing layer is needed, whether anti-fog performance is required, the destination market for compliance, and the target roll width, roll diameter, core and thickness. With those inputs, a material recommendation and a sample roll plan can be prepared. To start, contact Carrie at operation01@pulixin.com or +86 13818585204 (WhatsApp: +86 13818585204), or download the product catalogue below.
Conclusion
Fogging on a refrigerated food tray is a specification problem before it is a material problem. The converters who solve it permanently do three things: they document the real cold chain, they declare anti-fog and moisture requirements in writing instead of hoping the sheet covers them, and they fix the sealing structure and roll-format acceptance criteria before the order is placed. Everything else — clarity, stiffness, forming stability — follows from those decisions.
For meat, fruit and vegetable, and prepared chilled-food tray projects, the sheet specification is where clarity, compliance and cost are decided at the same time. Getting it right in one document is cheaper than discovering it in a retail case.
Specify your refrigerated tray sheet roll with PULIXIN
PULIXIN supplies PET, PP, PS and HIPS thermoforming plastic sheet rolls, including food-grade, anti-fog, high-stiffness and multilayer co-extruded options, with customized thickness, width, colour and roll format for roll-fed thermoforming lines.
Request a sample roll or a specification review: Carrie · operation01@pulixin.com · +86 13818585204 (Tel / WhatsApp)
Address: No.32 Lubin Rd, Luyuan Industrial Zone, Pudong, Shanghai, China
Website: www.pulixin.com
Product catalogue: PULIXIN Catalogue (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.